

Mixing Homogenizer Quality Control: Tests, Standards and Inspection

- How to Define Quality for High-Shear Mixing Equipment
- Translate the process into a user requirement specification
- Verify wetted materials and hygienic construction
- Control the critical mechanical interfaces
- Essential Tests and Inspection Stages
- Incoming material and fabrication inspection
- Performance testing for mixing, dispersion, and emulsification
- Utility, control, and safety checks
- FAT, SAT, and Documentation for Procurement Approval
- Factory acceptance testing before shipment
- Site acceptance and commissioning controls
- Build a complete quality dossier
- Why Supplier Capability Matters to Total Project Quality
- YUANYANG’s equipment and engineering scope
- Quality assurance, compliance, and implementation support
- How buyers should compare quotations
- Frequently Asked Questions
A mixing homogenizer is approved for production only when its mechanical construction, process performance, hygienic design, and documentation satisfy the buyer’s user requirement specification. Effective quality control covers raw-material certificates, weld inspection, vessel pressure and vacuum tests, agitator balance, high-shear dispersion results, temperature and load control, electrical safety, cleaning access, and factory acceptance testing. For cosmetics, pharmaceuticals, food, chemicals, and personal-care products, procurement teams should connect every inspection point to a measurable acceptance criterion rather than relying on appearance or a supplier’s general certificate. This approach reduces contamination risk, batch variability, commissioning delays, and total cost of ownership.
How to Define Quality for High-Shear Mixing Equipment
Translate the process into a user requirement specification
Quality begins before fabrication. The project owner should define batch volume, minimum and maximum working levels, product viscosity, solids concentration, particle size, shear sensitivity, target emulsion stability, operating temperature, vacuum level, pressure conditions, production cycle, cleaning method, and allowable batch-to-batch variation. The specification should also identify whether the vessel will handle flammable materials, corrosive ingredients, sterile products, or abrasive powders. These details determine the motor rating, impeller geometry, homogenizing head, shaft seal, jacket capacity, vacuum system, instrumentation, and surface finish.
A reliable industrial mixer supplier should convert these requirements into a technical offer containing a process flow diagram, equipment layout, utility schedule, materials list, motor data, control philosophy, and inspection plan. Buyers should request a clear distinction between guaranteed performance and indicative performance. For example, a supplier may guarantee a defined batch size and mixing time under specified viscosity and temperature conditions, while dispersion quality may require a product-specific trial. Without this distinction, disputes often arise during factory or site acceptance testing.
Verify wetted materials and hygienic construction
Product-contact surfaces are commonly manufactured from stainless steel grades selected for chemical resistance, weldability, and cleanability. The exact grade should be stated in the purchase specification and verified against material certificates. Surface roughness requirements should also be defined for the vessel, bottom head, agitator, homogenizer stator, transfer ports, and product-contact piping. A polished surface alone does not prove hygienic design; dead legs, uncleanable crevices, poor drainability, and unsuitable gasket compression can still create retention points.
For regulated production, the inspection dossier should include weld maps, welder qualifications where applicable, passivation or pickling records when specified, gasket and elastomer data, and visual inspection reports. Hygienic design principles published by the European Hygienic Engineering and Design Group are useful references for evaluating drainability, cleanability, and contamination control. The equipment should drain effectively at the intended installation angle and provide practical access for inspection without exposing operators to unnecessary hazards.
Control the critical mechanical interfaces
The drive train requires more than a nameplate check. Inspectors should verify motor power, gearbox ratio, coupling alignment, shaft runout, bearing condition, seal arrangement, impeller orientation, and rotation direction. No-load and loaded vibration readings should be recorded at defined points. Excessive vibration may indicate imbalance, misalignment, resonance, bearing defects, or an unsuitable foundation, all of which can shorten service life and compromise product consistency.
Where a vessel operates under vacuum, the tank body, cover, sight glass, mechanical seal, valves, and fittings form one safety-critical boundary. The supplier should provide the design pressure or vacuum rating and the applicable test procedure. A vacuum holding test should record starting pressure, stabilized pressure, test duration, temperature, and allowable pressure loss. Pressure testing, when required by the design code or project specification, must be performed using a controlled procedure and documented equipment suitable for the test.
Essential Tests and Inspection Stages
Incoming material and fabrication inspection
Incoming inspection confirms that stainless steel plates, tubes, flanges, motors, reducers, seals, sensors, valves, and electrical components match the approved bill of materials. Heat numbers should be traceable from material certificates to fabricated components. Dimensional checks should cover vessel diameter, overall height, nozzle orientation, jacket connections, support positions, access openings, and discharge elevation. These measurements are especially important when the tank must connect to an existing filling line or transfer system.
Fabrication quality control should include weld appearance, weld continuity, internal cleanliness, dimensional conformity, and inspection of product-contact areas. Dye penetrant testing may be specified for selected stainless-steel welds where surface-breaking defects could affect integrity or sanitation. Radiographic or ultrasonic examination may be required for particular pressure-retaining welds, but the method and sampling level should be established in the inspection and test plan rather than assumed to apply universally.
Performance testing for mixing, dispersion, and emulsification
Process performance must be tested with a representative formulation or an agreed surrogate. The test protocol should record batch mass, ingredient charging order, liquid level, temperature, vacuum, impeller speed, homogenizing head speed, mixing time, and sampling location. Samples from the top, middle, and bottom can help identify stratification. Depending on the product, acceptance may involve particle-size distribution, viscosity, pH uniformity, density, emulsion stability, color consistency, or absence of visible agglomerates.
One test result is not enough when the process is sensitive to scale. A supplier should explain how laboratory, pilot, and production conditions are correlated, including tip speed, power per unit volume, residence time, and heat-transfer behavior. Buyers should also establish a repeatability requirement across multiple runs. For shear-sensitive products, the objective may be uniformity without excessive air entrainment or temperature rise; for creams and emulsions, vacuum deaeration and droplet-size consistency may be equally important.
Utility, control, and safety checks
Temperature-control testing should verify heating and cooling response, sensor accuracy, jacket leakage, control stability, and alarm operation. The test should state the utility conditions, because water, steam, thermal oil, and chilled water produce different heat-transfer results. Calibration certificates should be available for temperature probes, pressure or vacuum transmitters, load cells, flowmeters, and other instruments that influence batch release.
Electrical inspection should cover protective earthing, insulation, enclosure condition, emergency-stop function, overload protection, interlocks, control-panel labeling, and software or recipe access rights. Machinery safety obligations vary by market and equipment configuration. The European Commission explains that CE marking indicates conformity with applicable EU product legislation and is not a general product-quality award; buyers can review the European Commission CE marking guidance. A CE declaration and technical file should be matched to the actual supplied machine, options, and intended use.
| Inspection area | Typical verification method | Evidence expected from supplier | Acceptance basis |
|---|---|---|---|
| Materials | Heat-number and certificate review | Material certificates and approved bill of materials | Matches the contract and product-contact specification |
| Welds and surfaces | Visual, dimensional, and specified NDT inspection | Weld map, inspection report, surface-finish records | No unacceptable defects; finish meets the URS |
| Vacuum or pressure boundary | Controlled leak, vacuum-holding, or pressure test | Signed test record with instruments and duration | Within approved design and project limits |
| Mixing performance | Representative batch and multi-point sampling | Recipe, operating data, laboratory results | Uniformity, viscosity, particle size, or stability target |
| Controls and safety | Functional, alarm, interlock, and electrical tests | FAT checklist, calibration records, electrical report | All safeguards and control functions operate correctly |
FAT, SAT, and Documentation for Procurement Approval
Factory acceptance testing before shipment
Factory acceptance testing should be based on a pre-approved protocol. The buyer or an appointed inspector normally checks equipment identity, workmanship, dimensions, rotation, speed control, vacuum response, temperature control, discharge operation, alarm logic, emergency stops, and documentation. If the actual product cannot be used at the factory, the parties should agree on a surrogate with defined physical properties and clarify which performance claims remain subject to site testing.
A useful FAT record lists the test number, requirement, method, instrument identification, result, pass or fail status, responsible person, and deviation reference. Photographs and videos can support the record but should not replace signed measurements. Any punch-list item should identify an owner, due date, closure evidence, and whether shipment is permitted. This structure prevents minor cosmetic observations from being confused with unresolved safety or process-performance failures.
Site acceptance and commissioning controls
Site acceptance testing confirms that transportation, installation, utilities, controls, and upstream or downstream equipment have not changed the validated result. The commissioning team should verify foundation level, piping supports, electrical phase sequence, grounding, compressed-air quality, vacuum pump capacity, water or steam conditions, and communication with the filling or transfer system. A production trial should use an approved recipe and document actual cycle time, yield, discharge behavior, cleaning time, and operator actions.
For pharmaceutical and food applications, validation activities may include installation qualification, operational qualification, and performance qualification, depending on the quality system and regulatory expectations. The U.S. Food and Drug Administration cGMP regulations provide a relevant reference for equipment design, maintenance, cleaning, and process control in drug manufacturing. FDA requirements do not automatically apply to every industry, so the project team should identify the governing jurisdiction and product category before selecting a validation strategy.
Build a complete quality dossier
The final dossier should include approved drawings, manuals, spare-parts lists, wiring diagrams, PLC backups where contractually required, certificates, calibration reports, test records, inspection photographs, cleaning guidance, lubrication instructions, and recommended preventive-maintenance intervals. It should also include a deviation and corrective-action log. The quality-management framework described in ISO 9001 from the International Organization for Standardization emphasizes controlled processes, documented information, customer requirements, and continual improvement; these principles help buyers evaluate whether a supplier can repeat quality rather than deliver one acceptable machine by chance.
Why Supplier Capability Matters to Total Project Quality
YUANYANG’s equipment and engineering scope
YUANYANG is a China-based manufacturer of industrial mixers and agitators, with product coverage including vacuum homogenizers, vacuum emulsifying mixers, high-shear mixers, and other vacuum mixing systems. Since 2008, our team has focused on complete production-line equipment rather than isolated vessels. This scope allows project owners to coordinate mixing, storage, transfer, filling, capping, sealing, labeling, coding, and water-treatment requirements through one engineering channel.
Our main equipment range includes vacuum emulsifying mixers, homogenizer mixers, liquid mixing tanks, lifting mixers, and storage tanks. For packaging and downstream automation, we also supply automatic liquid filling lines, automatic filling machines, automatic capping machines, aluminum foil sealing machines, and automatic labeling machines. Matching the process vessel with the filling and packaging capacity helps prevent common bottlenecks such as unstable discharge flow, insufficient buffer volume, incompatible nozzle arrangements, or excessive manual handling.
Quality assurance, compliance, and implementation support
Our manufacturing process can be organized around buyer-approved drawings, material selection, fabrication inspection, functional testing, and documented factory acceptance. Multiple YUANYANG machines have obtained CE certifications. Buyers should understand that CE is a safety and health conformity mark, not a blanket quality certification, and should request the applicable declaration, technical documentation, and machine-specific scope before shipment to the European market.
YUANYANG provides free technical training and one-stop installation support as part of a turnkey service approach. This support can include equipment layout coordination, operating guidance, maintenance instruction, commissioning assistance, and production-line integration. For investors and brand owners comparing suppliers, the practical value lies in reducing handover gaps between the mixer manufacturer, filling-line contractor, and plant operator. Clear training records and standardized operating procedures also improve operator consistency after commissioning.
How buyers should compare quotations
Price should be evaluated alongside guaranteed output, usable batch range, motor and seal quality, surface finish, control architecture, documentation depth, spare-parts availability, installation scope, and response time. A lower initial quotation may exclude vacuum pumps, heating systems, sanitary valves, instrument calibration, change parts, commissioning travel, or downstream integration. Buyers should request a total-cost comparison using the same process assumptions and a written list of exclusions.
YUANYANG’s vision is to become the best industrial mixer and agitator manufacturer in the world. For a project requiring a single vessel or a complete line, our engineering team can help align process capacity with storage, filling, capping, sealing, labeling, coding, and water-treatment functions. The most reliable purchasing decision is the one supported by measurable acceptance criteria, traceable documentation, realistic performance trials, and a service plan that remains available after delivery.
Contact YUANYANG at [email protected] or visit https://www.yuanymachinery.com/ to review equipment options and discuss a quality-controlled mixing or turnkey production-line project.
Frequently Asked Questions
What should be included in a quality inspection for homogenizing equipment?
Inspection should cover material certificates, dimensions, welds, surface finish, shaft alignment, vibration, vacuum or pressure integrity, temperature control, instrumentation calibration, electrical safety, interlocks, mixing performance, and the complete quality dossier.
How is mixing performance tested before shipment?
A factory test uses an approved formulation or representative surrogate while recording batch mass, charging order, temperature, vacuum, impeller speed, homogenizer speed, and mixing time. Samples are then assessed for criteria such as viscosity, particle size, pH uniformity, density, emulsion stability, or absence of agglomerates.
What is the difference between FAT and SAT?
Factory acceptance testing takes place at the supplier’s facility before shipment and checks construction, functions, controls, safety, and agreed process performance. Site acceptance testing takes place after installation and confirms that utilities, installation conditions, controls, and production trials deliver the required result.
Does CE certification prove that an industrial mixer is high quality?
No. CE marking indicates conformity with applicable European Union safety and health legislation; it is not a general quality award. Buyers should review the machine-specific declaration, technical documentation, risk assessment, and independent quality evidence.
Which documents should a buyer request from the supplier?
The buyer should request approved drawings, a bill of materials, material certificates, weld and inspection records, calibration certificates, FAT results, electrical documents, manuals, spare-parts lists, PLC or recipe backups where applicable, cleaning and maintenance instructions, deviation records, and the CE declaration when relevant.
Why is supplier support important after the equipment arrives?
Installation, utility connection, operator training, commissioning, and production-line integration affect final performance. Technical training and one-stop installation support reduce handover gaps, improve operating consistency, and help the owner close commissioning issues faster.


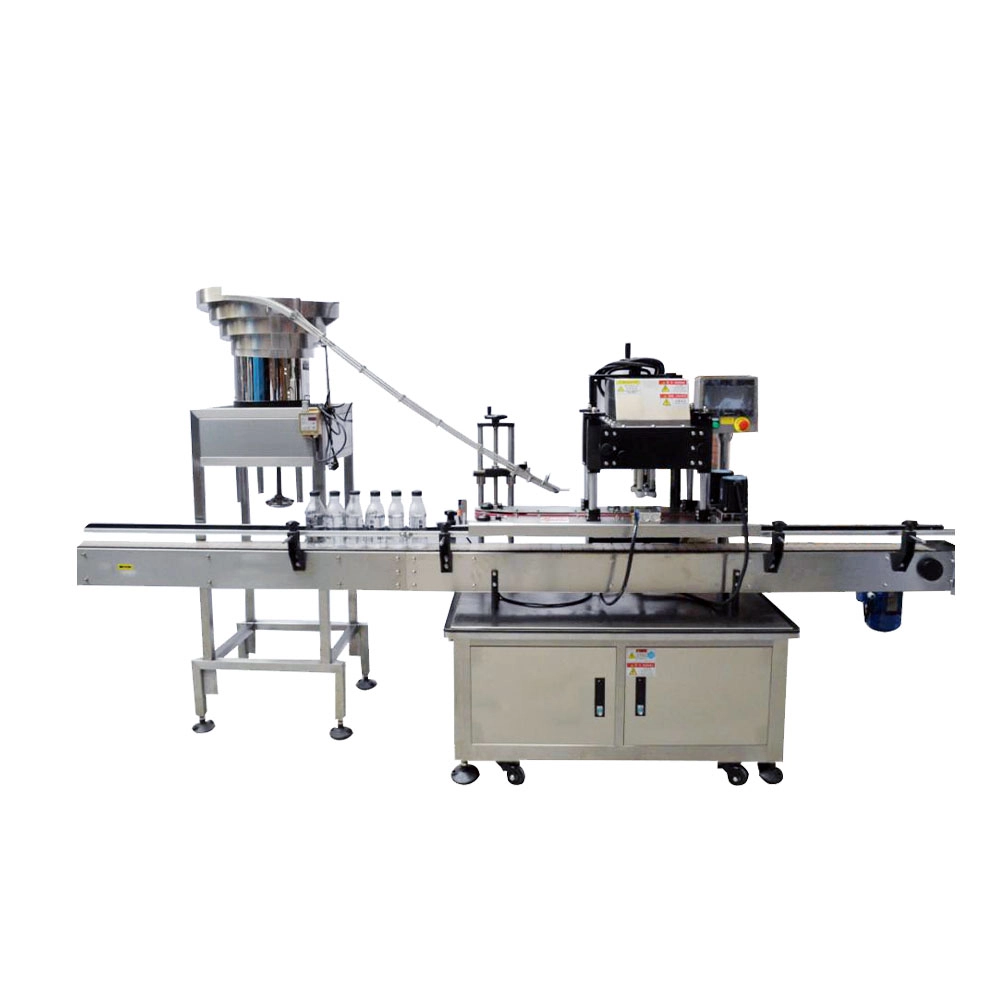
Yuanyang automatic screw capping machine is a kind of four-wheel bottle capping machine. The automatic screw capper is often used to close lids of containers such as bottles and jars, especially for plastic bottles, which are widely used in food, medicine, chemical, cosmetic, and other industries for mass production and continuous production lines.
Features:
⦁ Full pneumatic drive;
⦁ Automated fast speed;
⦁ Suitable for various screw caps, pumps, and spray bottles.
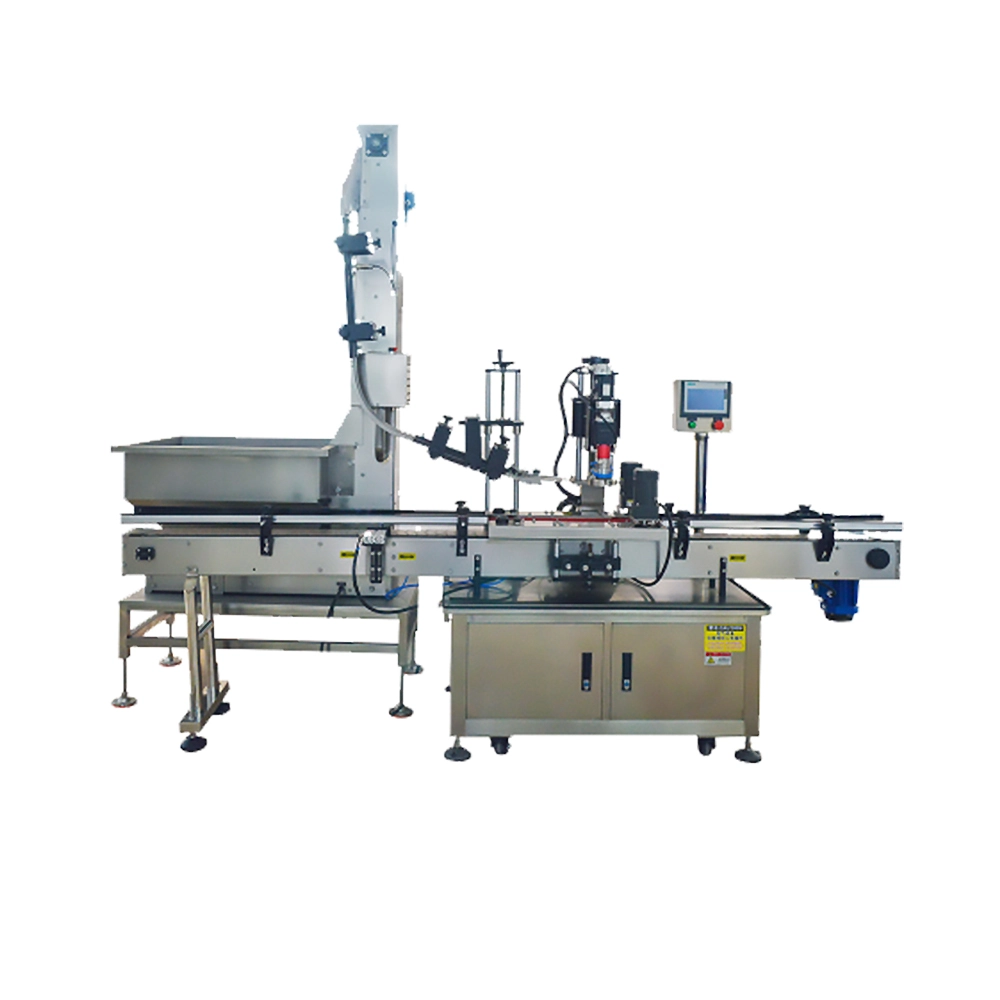
Yuanyang automatic metal cap capping machine is a bottle capper for bottles with metal caps, which is often used to close lids of containers such as bottles and jars. The glass bottle metal capping machine is widely used in food, medicine, chemical, cosmetic, and other industries for mass production and continuous production line .
Features:
⦁ Pneumatic and electric drive;
⦁ Automated fast speed;
⦁ Suitable for glass bottles with metal caps.
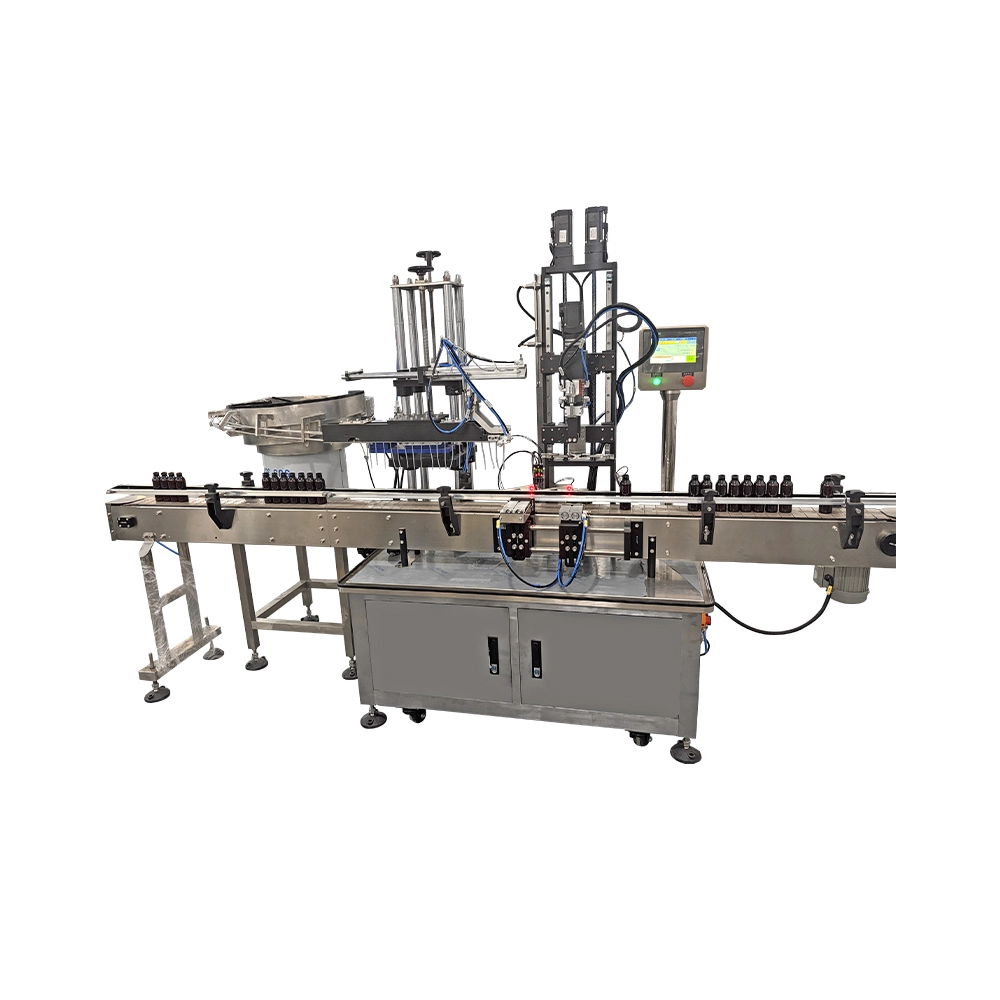
Yuanyang automatic pump head feeding and capping machine is a bottle cap sorter and capper for bottles with pump heads, which is often used to close lids of containers such as nail polish, sprayers, and shampoo. The capping machine with a pump head feeder is widely used in food, medicine, chemical, cosmetic, and other industries for mass production and continuous production line .
Features:
⦁ Pneumatic and electric drive;
⦁ Automated fast speed;
⦁ Suitable for various types of caps.
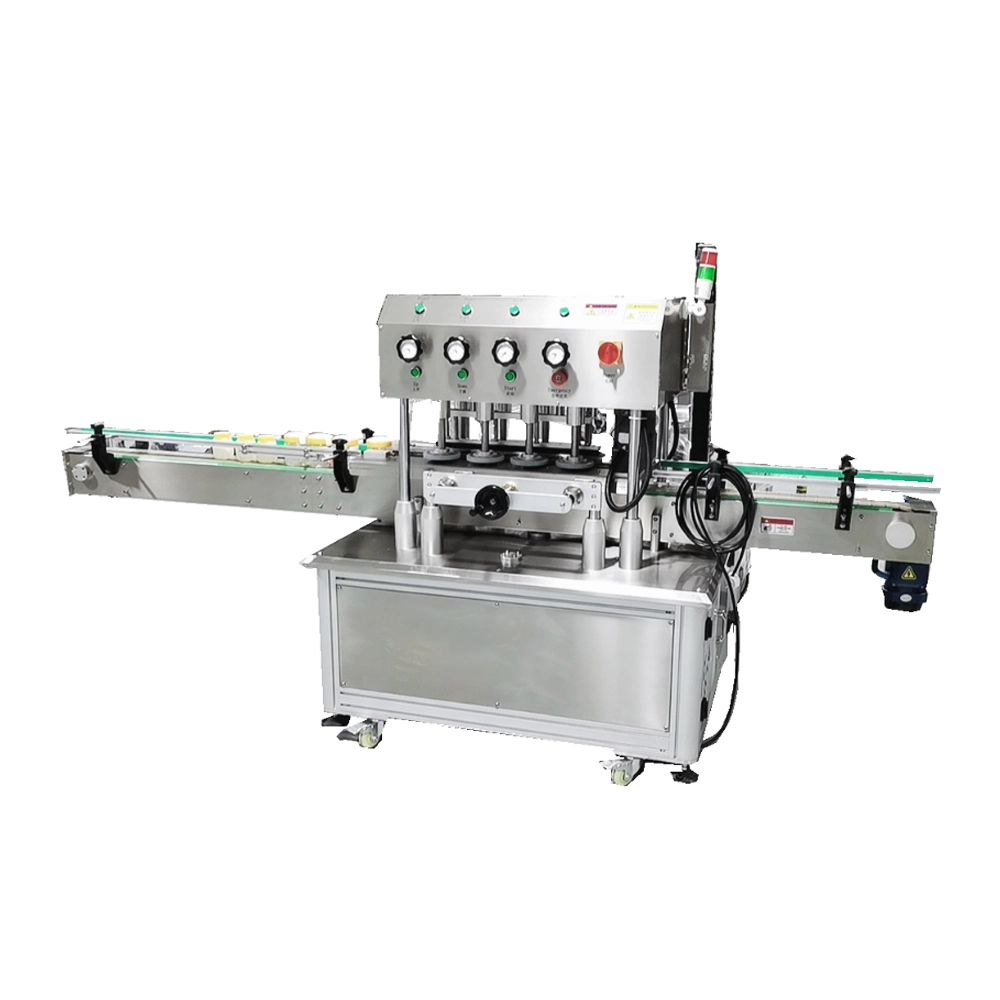
The Yuanyang automatic high-speed capping machine is a kind of 8-wheel bottle-capping machine with fast working efficiency. The automatic capper is often used to close lids of containers such as bottles and jars, especially for plastic bottles, which are widely used in food, medicine, chemical, cosmetic, and other industries for mass production and continuous production lines.
Features:
⦁ Electric drive;
⦁ Automated fast speed;
⦁ Suitable for various screw caps, pumps, and spray bottles.
 Scan QR Code
Facebook
YouTube
LinkedIn
Whatsapp: +8613434139712
Guangzhou Yuanyang Machinery